Home / Guides / Hygienic design
HYGIENIC DESIGN · EHEDG GUIDELINE 8 · R638 REGULATION 7
Key facts
- Core reference EHEDG Guideline 8, Hygienic Design Principles
- Minimum internal radius 3 mm at any angle of 135 degrees or less
- Recommended surface finish Ra 0.8 micrometres or better on stainless product contact
- Minimum slope 3 degrees, no horizontal surfaces
- South African law R638 of 2018, regulation 7, equipment and containers
- Legal surface limit after cleaning 100 viable micro-organisms per cm2
- Scheme clauses FSSC 22000 2.5.15, BRCGS 4.6, IFS 4.17, SQF Edition 9 Module 11
- Machinery standards EN 1672-2:2020, EN ISO 14159:2008
- Entry level course Hygienic Design Essentials, R1 350, 5 hours
- Free tool in this guide the 30 point hygienic design walk
Learn to read a machine, not just clean it
Hygienic Design Essentials takes a QA officer, hygiene manager, fitter or supervisor from never having heard of EHEDG to walking a line and naming the faults, in five hours. It is one of the very few hygienic design courses written for the people who meet the machine rather than the people who draw it.
Enrol in Hygienic Design Essentials, R1 350
See all hygienic design courses
Self paced online with lifetime access. Five hours. Fifteen lessons, a thirty point line walk, a marked assignment and a QR verified Certificate of Achievement. No discount codes on this course.
What is hygienic design, and what is it not?
Hygienic design is the design of equipment, utensils, pipework and the building itself so that product residue and microorganisms cannot enter places you cannot reach, cannot collect in those places, and cannot survive the cleaning and disinfection that follows. It is a design control. You buy it once, or you fail to buy it once, and then you live with that decision for the fifteen years the machine is on your floor.
Three questions settle almost every argument on the floor:
- Can soil get in there?
- Once it is in, can it collect and stay?
- Can the cleaning method you actually use reach it and take it out again?
If the answer to the third question is no, you do not have a cleaning problem. You have a machine that cannot be cleaned, and no amount of scrubbing, no stronger chemical and no extra shift will change that.
It is worth being clear about what hygienic design is not. It is not the same as stainless steel. A 316 stainless frame with an open tube end is a worse harbourage than a sealed plastic one. It is not the same as a shiny finish, because a mirror polished surface with a hairline crack in the weld is still a failure. It is not a certificate you buy with the machine, because EHEDG certification applies to specific equipment types tested against specific protocols, not to a whole plant. And it is not the cleaning team’s responsibility. By the time the cleaning team meets the fault, the decision that created it was made months earlier by somebody holding a purchase order.
Why cleaning cannot correct a design fault
Cleaning is a repeated control. It happens every shift, it is done by people under time pressure, and it is verified by swabs and visual checks. Design is a single control that either works or does not, silently, for years.
The problem is what sits between the two. A crevice does not need to be visible to matter. A flat gasket that is compressed correctly on day one can open a measurable gap once it has been cycled between cleaning temperature and process temperature a few hundred times, because elastomers expand more than twenty times as much as stainless steel for the same change in temperature. Industry guidance puts the gap that a five millimetre PTFE gasket can open under that cycling in the order of tens of micrometres. That is invisible to an inspector standing at the machine, and it is an enormous space to a bacterial cell about one micrometre long.
Once cells are in a space that cleaning solution does not exchange, they attach, they produce extracellular polymeric substance, and within days they are living in a biofilm that resists both detergent and disinfectant far better than the same organisms in suspension. That is the mechanism behind the phrase every environmental monitoring programme eventually runs into: the same positive, in the same place, month after month, on a line that is being cleaned properly.
South Africa has the most expensive possible reminder of what persistence in a plant costs. The 2017 to 2018 listeriosis outbreak, the largest ever recorded anywhere, ran to 1 060 laboratory confirmed cases and 216 deaths according to the National Institute for Communicable Diseases and the World Health Organization. Listeria monocytogenes does not persist in a plant because somebody skipped a cleaning shift. It persists because there is somewhere in that plant it can live: a hollow frame that was drilled and tapped, a floor drain surround that was never sealed, a bearing housing inside the product zone, a conveyor end cap pushed into an open tube. Those are all design decisions.
You cannot clean your way out of a crevice. You can only stop buying them.The line we open the course with, and the one delegates quote back to us most often
What does South African law actually say about equipment?
Most people in South African food manufacturing know regulation R638 of 2018 as the Certificate of Acceptability regulation. It is a great deal more than that, and regulation 7 is the part almost nobody quotes.
Regulation 7, Standards and Requirements for Food Containers, Appliances and Equipment, requires that containers and appliances must not yield any unwholesome, injurious or toxic substance, that their surfaces must be of smooth, rust proof, non toxic and non absorbent material that is free of open joints or seams, and that equipment must not be used for handling food if it is not clean or if it is chipped, split or cracked. It then sets a number that very few sites test against: after cleaning, food contact surfaces must not carry more than 100 viable micro-organisms per square centimetre.
Read that again. Free of open joints or seams is a hygienic design requirement, written into South African law, applying to every food premises with a Certificate of Acceptability. It is not a scheme, it is not voluntary, and an environmental health practitioner is entitled to look at your butt welded lap joint and your bolted bracket and form a view.
Regulation 5 and regulation 6 do the same job for the building: interior wall, ceiling and floor surfaces of smooth, rust free, non toxic, cleanable and non absorbent material that is dust proof and water resistant, natural ventilation of at least five percent of the floor area, lighting of at least 200 lux where it is artificial, and an approved waste water and refuse arrangement. If you want the wider picture of what R638 requires, our guide to the Certificate of Acceptability walks through the whole regulation.
The ten rules of hygienic design, with the actual numbers
EHEDG Guideline 8 is the reference every other hygienic design document builds on. The table below is how we teach it: ten rules, each with the number if there is one, and the source so you can defend it in a specification meeting. The section numbers are from the third edition of 2018. A fourth edition was released in December 2025 and may renumber sections, so cite the edition you hold.
| # | The rule | The number or the test | Where it comes from |
|---|---|---|---|
| 1 | Materials | Food contact materials must be non toxic, corrosion resistant, non absorbent and stable in the cleaning chemicals you actually use, at the temperatures you actually use | EHEDG GL8 section 5; EC 1935/2004; R638 reg 7 |
| 2 | Surface finish | Ra of 0.8 micrometres or less recommended on stainless product contact, roughly a 180 to 240 grit polish. Avoid pores, sharp peaks, deep valleys, crevices and cracks | EHEDG GL8 section 6.2 |
| 3 | Radii | All internal angles of 135 degrees or less need a minimum radius of 3 mm. Sharp corners of 90 degrees or less must be avoided | EHEDG GL8 section 6.2; EN 1672-2 |
| 4 | Drainability | Interior and exterior must be self draining or drainable. No horizontal surfaces. Slope at least 3 degrees to one side | EHEDG GL8 section 6.4 |
| 5 | Dead spaces | No area where microorganisms can harbour and grow. Where a gasket or membrane separates product from a potential dead space, visual leak detection at the lowest possible point | EHEDG GL8 sections 4.3 and 6.2 |
| 6 | Seals | Static seals shall be front flush when installed. O-rings in product contact are limited to static duty. Crevice free design demonstrated by testing, not by assertion | EHEDG GL8 section 6.2; EHEDG Doc 16 |
| 7 | Joints and welds | No metal to metal joints in product contact other than welding. Product contact welds continuous and free of imperfections, and welds on the non product side continuous as well | EHEDG GL8 section 6.3; Docs 9 and 35 |
| 8 | Fasteners | Eliminate exposed screw threads, fastener metal to metal joints, pockets such as cap head screws and pop rivets, and crevices in hinges. Nothing that can loosen and fall into product | EHEDG GL8 sections 6.2 and 4.5 |
| 9 | Hollow bodies and steps | Hollow structures sealed and never penetrated by a drilled and tapped fixing. Avoid steps caused by misalignment of equipment and pipe connections | EHEDG GL8 sections 6.2 and 6.6 |
| 10 | Installation | Sealed to the floor with no pockets or gaps, or clear of it, with floor contact points minimised, enough clearance from walls and ceilings for cleaning and inspection, and no condensate falling onto product contact surfaces | EHEDG GL8 section 6.6 |
Two honest notes on those numbers, because the internet repeats a lot of figures that are not in the guideline. First, EHEDG Guideline 8 contains no length to diameter figure for dead legs. The commonly quoted L over D of 1 comes from the closed equipment guideline, and the 3-A figure of 2 with a 127 mm cap is a different document again. Second, the 6 mm radius that many specifications still call up is the 2004 preferred value; the current guideline keeps only the 3 mm minimum, and 6 mm survives in industry guidance for weld fillets in the food area. When you write a specification, say which document and which edition you are calling up.
See the ten rules on real equipment, not on slides
Module 2 of Hygienic Design Essentials takes each rule onto a chilled ready meal line, a dairy CIP circuit and a meat processing brownfield project, with fourteen drawn diagrams and a scored game after every module.
Start Hygienic Design Essentials
Browse the hygienic design pathway
Four modules, fifteen lessons, 213 assessment questions and a downloadable learner manual.
Food area, splash area, non food area: the three zones that decide how hard a rule bites
Not every rule applies everywhere with the same force, and this is where most site arguments start. EN 1672-2 splits equipment surfaces into three areas, and EHEDG uses the same logic.
| Area | What it means | What that does to the rules |
|---|---|---|
| Food area | Surfaces in contact with product, and surfaces from which product or drip returns to the product stream | Every rule applies at full strength. This is where 3 mm radii, front flush seals, continuous welds and Ra 0.8 micrometres are not negotiable |
| Splash area | Surfaces that product touches or splashes onto but from which it does not return to the product stream | Cleanability still governs, because splash area soil becomes aerosol and becomes hands. Exposed threads, open tube ends and horizontal ledges are still faults here |
| Non food area | Surfaces with no product contact and no realistic route back to product | Design for cleanability of the outside and for pest exclusion, but the hard numbers do not apply. Being sealed is what makes a space non food area in the first place |
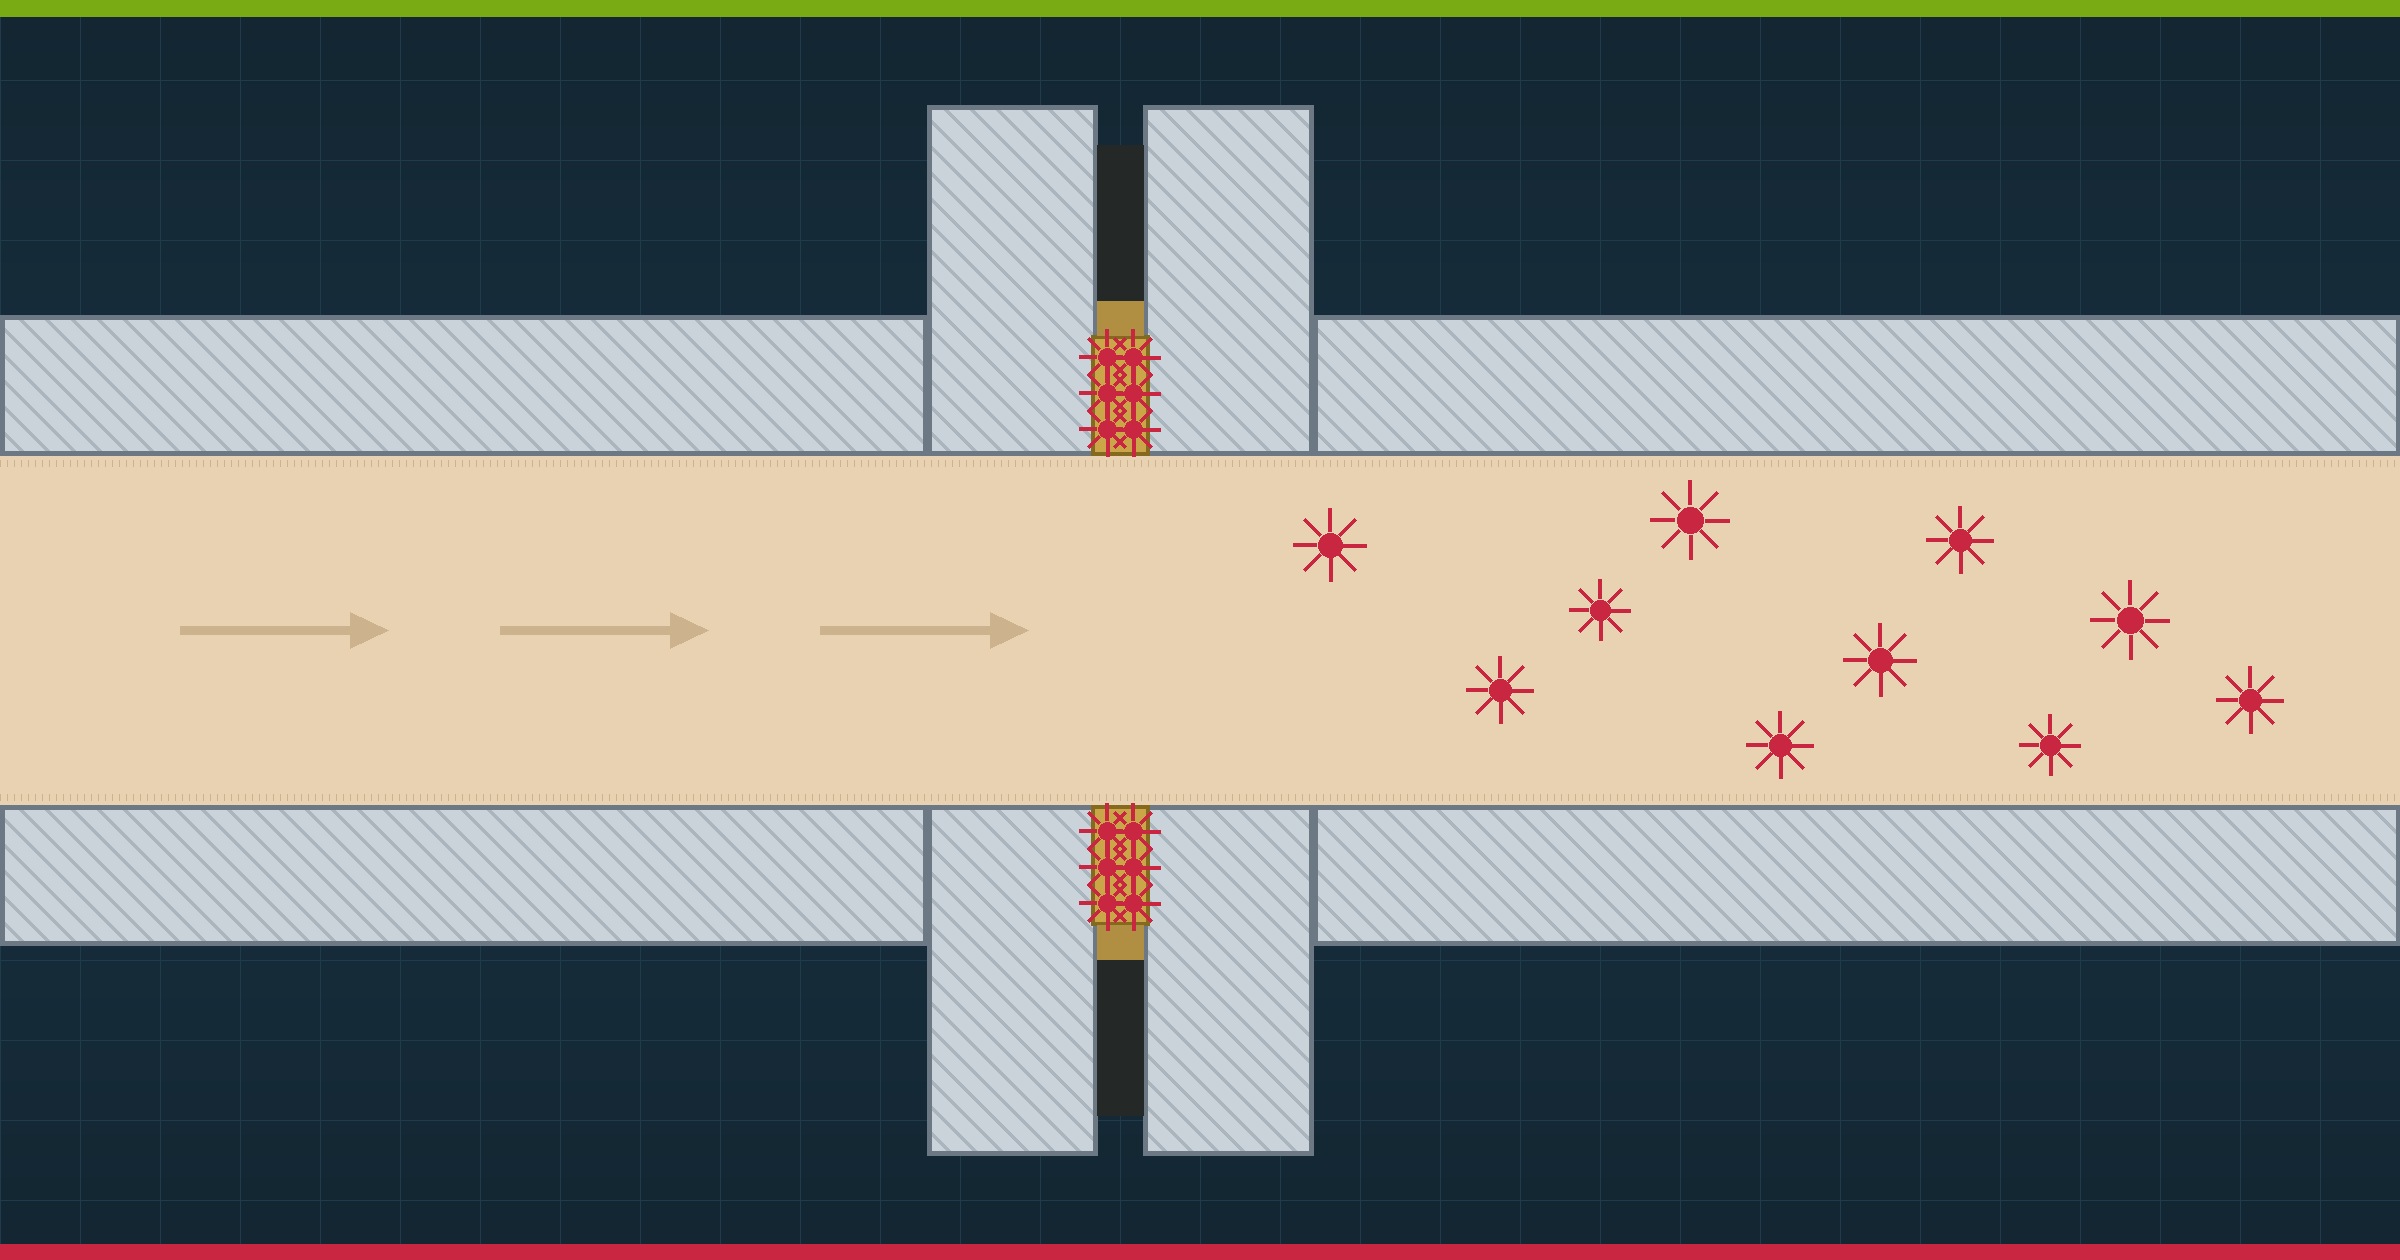
A worked example we argue out in the course: a square section conveyor frame with a push in plastic end cap. The outer faces of that cap are splash area, because wash down water and product debris land on them. The inside of the tube is only non food area if the tube is genuinely sealed. A push in cap is not a seal. It is a lid on a harbourage, and the day somebody knocks it out with a pallet jack you have an open pipe running the full length of your line at product height.
The second thing the zones decide is whether the equipment is open or closed. Open equipment, the kind the EHEDG type EL Class I and Class II tests apply to, has product surfaces exposed to the room and depends on manual or foam cleaning. Closed equipment is cleaned in place, and its whole risk sits in whether the cleaning solution actually reaches every internal surface at the right velocity, temperature and time. A dead leg in a closed system is invisible in a way that a dirty conveyor never is.
Six design faults you can find on your own line this week
You do not need a drawing set or a consultant to start. Take a torch, a mirror, a phone camera and thirty minutes on a clean, stopped, isolated line. These six turn up on almost every site we walk.
Walk the line and look for these
- Open or capped hollow frames. Square tube legs and cross members with an open end, a push in plastic cap, or a drilled and tapped bolt through the wall of the tube. Shine the torch inside.
- Exposed threads in a splash area. Bolts standing three or four threads proud of the nut, wing nuts, pop rivets, self tapping screws and split pins anywhere product can splash.
- A gasket that is not front flush. Run a fingernail across the joint. If it drops into a groove or catches on a lip, there is a step, and a step is a crevice with a nicer name.
- Horizontal ledges that hold water. Guard rails, cable trays, motor plinths and control cabinet tops. If there is still a puddle twenty minutes after wash down, the slope is wrong.
- Long branches off a CIP line. Sample points, pressure gauges, drain valves and capped spare tees. If the branch is longer than its own diameter, flow will not scour it.
- Silicone where a gasket belongs. RTV sealant smeared into a leaking joint is a temporary repair that becomes permanent. It shrinks, it lifts at the edges, and it is the first place a swab goes positive.
Photograph each one with something in the frame for scale, write down the line, the position and what the fault is, and you have the beginning of an equipment improvement register. When you take those photographs into your next management review, you are no longer arguing about cleaning standards, you are arguing about capital, and that is a conversation that actually moves.
Use the free thirty point hygienic design walk on this site. It scores your line out of sixty, flags the priority zeros, and exports a spreadsheet you can hand to engineering. No sign up needed.
Which standards, schemes and regulations ask for hygienic design?
This is the table to take into a budget meeting when somebody says hygienic design is a nice to have. Every one of these is either law in South Africa or a clause your certification body will open.
| Document | Where hygienic design sits | What it asks for |
|---|---|---|
| R638 of 2018 (South Africa) | Regulation 7, and regulations 5 and 6 for the building | Smooth, rust proof, non toxic, non absorbent surfaces free of open joints or seams; not more than 100 viable micro-organisms per cm2 after cleaning |
| R908 of 2003 (South Africa) | HACCP regulation, for listed sectors | A fully implemented Codex based HACCP system; hygienic design is part of the prerequisite base that HACCP sits on |
| ISO 22000:2018 | Clause 8.2.4, prerequisite programmes | Suitability of equipment and its accessibility for cleaning, maintenance and preventive maintenance |
| FSSC 22000 (V6 and V7) | Additional requirement 2.5.15, Equipment Management | A documented purchase specification addressing hygienic design, with supplier evidence before installation, plus risk based change management with documented commissioning |
| BRCGS Food Safety Issue 9 | Clause 4.6, rewritten as a lifecycle | 4.6.1 specification and authorisation, 4.6.2 design and construction based on risk, 4.6.3 installation and commissioning, 4.6.4 mobile equipment. 4.6.2 is one of the most common minor non-conformances raised under Issue 9 |
| IFS Food Version 8 | Clause 4.17 Equipment, with 4.8 and 4.9 for layout and premises | Fitness for purpose, hygienic design of product contact construction, validation before use of new or modified equipment, condition monitoring and change management |
| SQF Edition 9 | Module 11, Site Location, Premises and Equipment | Premises construction, drainage, lighting, and equipment and utensils designed and installed to prevent food safety risks, using impervious materials |
| EN 1672-2:2020 | The machinery standard behind most of it | Food area, splash area and non food area, cleanability requirements and an iterative hygiene risk reduction process for machine builders |
| EN ISO 14159:2008 | Safety of machinery, hygiene requirements | Hygiene requirements for the design of machinery, currently under revision as ISO/DIS 14159 |
| EHEDG guidelines | Guideline 8 for the principles, then the equipment specific documents | The technical detail behind every clause above, including the numbers in this article |
The pattern is worth naming. Ten years ago the schemes asked whether your equipment was clean. They now ask whether you specified it correctly before you bought it, and whether you can produce the supplier evidence. That is a procurement and engineering question, and it is why the people who need this training are increasingly not in the QA office at all. If you are building the wider prerequisite base, our guide to prerequisite programmes and GMP covers what sits around it, and the FSSC 22000 V7 additional requirements guide covers clause 2.5.15 in its scheme context.
Why practical hygienic design training is so hard to find
Search for hygienic design training and you will find four kinds of thing, and a gap.
EHEDG runs its own training and it is genuinely excellent. It is also built for design engineers, is largely delivered in person, and is concentrated in Europe. Equipment suppliers run free webinars, which are useful and are also tied to the supplier’s own catalogue. Universities teach it inside process and mechanical engineering degrees, which is no help to somebody already ten years into a career. Consultants run in house workshops, which work well and cost what a plant visit costs.
What almost nobody writes is training for the people who actually meet the machine: the QA officer who swabs it, the hygiene manager who has to justify the same positive for the third month running, the fitter who is about to weld a bracket onto a frame tube, the production supervisor who signs the line off, and the buyer who is comparing two quotes where one machine is twenty percent cheaper for reasons nobody has explained. That is the gap, and it is why this is one of the few hygienic design courses on the internet that is fully online, self paced, priced for an individual rather than a corporate training budget, written in South African regulatory context, and built around walking a real line rather than reading a slide deck.
We are honest about the limits of that. ASC is not EHEDG, the course is not approved or endorsed by EHEDG or by any scheme owner, and finishing it does not make anyone a hygienic design engineer. What it does is make you able to read a machine, name what is wrong with it using the right words and the right clause, and write a purchase specification that stops the next one arriving with the same fault. For most food businesses, that is the step that was missing.
Where to start, in order
If you do nothing else after reading this, do these three things in this order.
- Walk one line. Use the thirty point walk. Score it. You will find between four and ten faults on a line nobody has ever looked at this way, and two or three of them will be things you can fix with a grinder and an hour.
- Fix your purchase specification. Most sites have no hygienic design wording in theirs at all, which means FSSC 22000 clause 2.5.15 is already a finding waiting to be written. One page, calling up EHEDG Guideline 8 and EN 1672-2 by edition, with the zones defined for your product, changes what arrives on your receiving bay.
- Train the people who meet the machine. Not just QA. The fitter, the supervisor and the buyer make more hygienic design decisions in a year than the QA manager does, and at the moment none of them have been told the rules.
Put your whole team through it for the price of one line stoppage
Hygienic Design Essentials is the foundation level of a three level pathway. Essentials teaches you to see the faults. The Intermediate and Advanced levels, releasing next, take you into specifying, testing and designing out. Sector versions for bakery, meat processing, dairy and beverage follow.
Enrol in Hygienic Design Essentials, R1 350
See all hygienic design courses
Teams of five or more can contact ASC for a group arrangement. No discount codes apply to the hygienic design series.
Frequently asked questions
What is hygienic design in simple terms?
Hygienic design is designing and installing equipment, pipework and buildings so that soil and microorganisms cannot get into them, cannot collect anywhere inside them, and cannot survive the cleaning that follows. It is a design control, not a cleaning control. Three questions settle almost every case: can soil get in, can soil collect there, and can the cleaning method actually reach it and remove it. If the answer to the last one is no, no amount of extra cleaning will fix the machine.
What is EHEDG Guideline 8?
EHEDG Guideline 8, Hygienic Design Principles, is the core reference document of the European Hygienic Engineering and Design Group. It sets out the general design principles that all the other EHEDG guidelines build on, including materials, surface finish, radii, drainability, dead spaces, seals, welds, fasteners and installation. The third edition was issued in 2018 and a fourth edition was released in December 2025. EHEDG is not a law and not a certification scheme, but its guidelines are the reference that food machinery builders, auditors and specifiers use when they say hygienic design.
What is the minimum radius for an internal corner in food equipment?
EHEDG Guideline 8 states that all internal angles of 135 degrees or less shall have a minimum radius of 3 mm, and that sharp corners of 90 degrees or less must be avoided. The older 2004 edition preferred a radius of 6 mm or larger with 3 mm as the minimum, and 6 mm is still widely used as the target for weld fillets in the food area in industry guidance. EN 1672-2 applies the same 3 mm minimum in the food area.
What surface finish does food contact stainless steel need?
EHEDG Guideline 8 recommends an Ra value of 0.8 micrometres or less on stainless steel product contact surfaces, achieved by mechanical polishing or machining, with higher values allowed for special equipment where cleanability is justified elsewhere. In practice that is a 180 to 240 grit polish. The wording is recommended rather than mandatory, and the more important requirement is the one next to it: avoid surface features that cannot be cleaned, such as pores, sharp peaks, deep valleys, crevices and cracks. A beautifully polished surface with a crack in it is still a failure.
Does South African law require hygienic design?
Yes, although it does not use the phrase. Regulation R638 of 2018, regulation 7, requires that food containers, appliances and equipment must not yield any unwholesome, injurious or toxic substance, that their surfaces be of smooth, rust proof, non toxic and non absorbent material that is free of open joints or seams, and that equipment must not be used if it is chipped, split or cracked. Regulation 7 also sets a hard number: after cleaning, food contact surfaces must not carry more than 100 viable micro-organisms per square centimetre. Free of open joints or seams is a hygienic design requirement written into South African law, and most people have never read it that way.
Which certification schemes require hygienic equipment design?
All of the GFSI benchmarked schemes now ask for it, and most of them ask at the point of purchase rather than at the point of failure. FSSC 22000 additional requirement 2.5.15 requires a documented purchase specification that addresses hygienic design, with supplier evidence before installation, plus risk based change management. BRCGS Food Safety Issue 9 clause 4.6 was rewritten into a lifecycle covering specification, construction, installation and commissioning. IFS Food Version 8 clause 4.17 covers hygienic design of product contact construction, validation before use and change management. SQF Edition 9 Module 11 covers premises and equipment construction. ISO 22000 clause 8.2.4 sits under all of them.
Is there a hygienic design course for people who are not engineers?
Very few, which is the gap ASC built for. EHEDG runs its own excellent training, but it is aimed at design engineers and is mostly delivered in person in Europe. Equipment suppliers run webinars tied to their own catalogues. Universities teach it inside engineering degrees. Almost nothing is written for the people who actually meet the machine every day: QA officers, hygiene managers, maintenance fitters, production supervisors and the person who signs the purchase order. Hygienic Design Essentials is written for exactly those people, with no engineering background assumed.
How long is the ASC Hygienic Design Essentials course and what does it cost?
Five hours in total, self paced and fully online, at R1 350 with lifetime access and no discount code. It is four modules and fifteen lessons, with a knowledge check and a scored game after every module, a thirty point hygienic design walk you run on your own line, a marked assignment and a final assessment. You get a QR verified Certificate of Achievement and a downloadable learner manual. It is the foundation level of a three level hygienic design pathway.
Hygienic Design Essentials for Food Industry Professionals, R1 350, 5 hours · Hygienic Design Intermediate, 9 hours, releasing next · Hygienic Design Advanced, releasing next
Browse every hygienic design course, see the hygienic design pathway on the course list, or run the free thirty point hygienic design walk on your own line. Related guides: prerequisite programmes and GMP, FSSC 22000 V7 additional requirements, food microbiology for non microbiologists and corrective action and root cause analysis.
ASC Food Safety Training · Leading with Science. Ensuring Food Safety. · Fully online, serving all of South Africa and beyond · info@ascfoodsafety.com · WhatsApp +27 61 483 0381 · SAATCA registered training centre (TC No. 065) · FoodBev SETA accredited provider No. 587/00337/1900 · B-BBEE Level 1 · Registered Lead Auditor (Exemplar Global and IRCA) · Consulting and document toolkits at ascfoodsafety.com