Home / Guides / Hygienic welding
HYGIENIC DESIGN · FABRICATION · PIPEWORK
Key facts
- What good looks like continuous, full penetration, smooth and flush, no crevices, pits, spatter or misalignment on the product side
- The finish to specify a roughness average of 0.8 micrometres is the widely used ceiling for product contact surfaces
- The method to ask for orbital TIG with inert gas purging on hygienic tube, with the machine’s weld log kept
- The evidence to demand numbered weld map, weld log, borescope inspection of an agreed sample, material certificates
- The documents behind it EHEDG guidance on welded joints, EN 1672-2 and ISO 14159 for machinery hygiene, 3-A practice in dairy
- Course pipework, couplings and welds are covered in Intermediate Hygienic Design, nine hours, R3 700
Write weld requirements a supplier cannot argue with
Intermediate Hygienic Design works through materials, welds, couplings, valves, tanks and CIP verification, with original engineering diagrams and narrated practical videos. Nine hours, online, self paced, lifetime access, certificate on completion.
See the Intermediate course, R3 700 →
R3 700 is the launch price. The standard price is R4 650.Why welds decide whether your line can be cleaned
Count the joints on one product line from tank to filler. On most plants the gasketed couplings number a few dozen, and the welds number in the hundreds. Every one of those welds has an inside surface that nobody has seen since the day it was made, and that surface is either smooth and continuous or it is not.
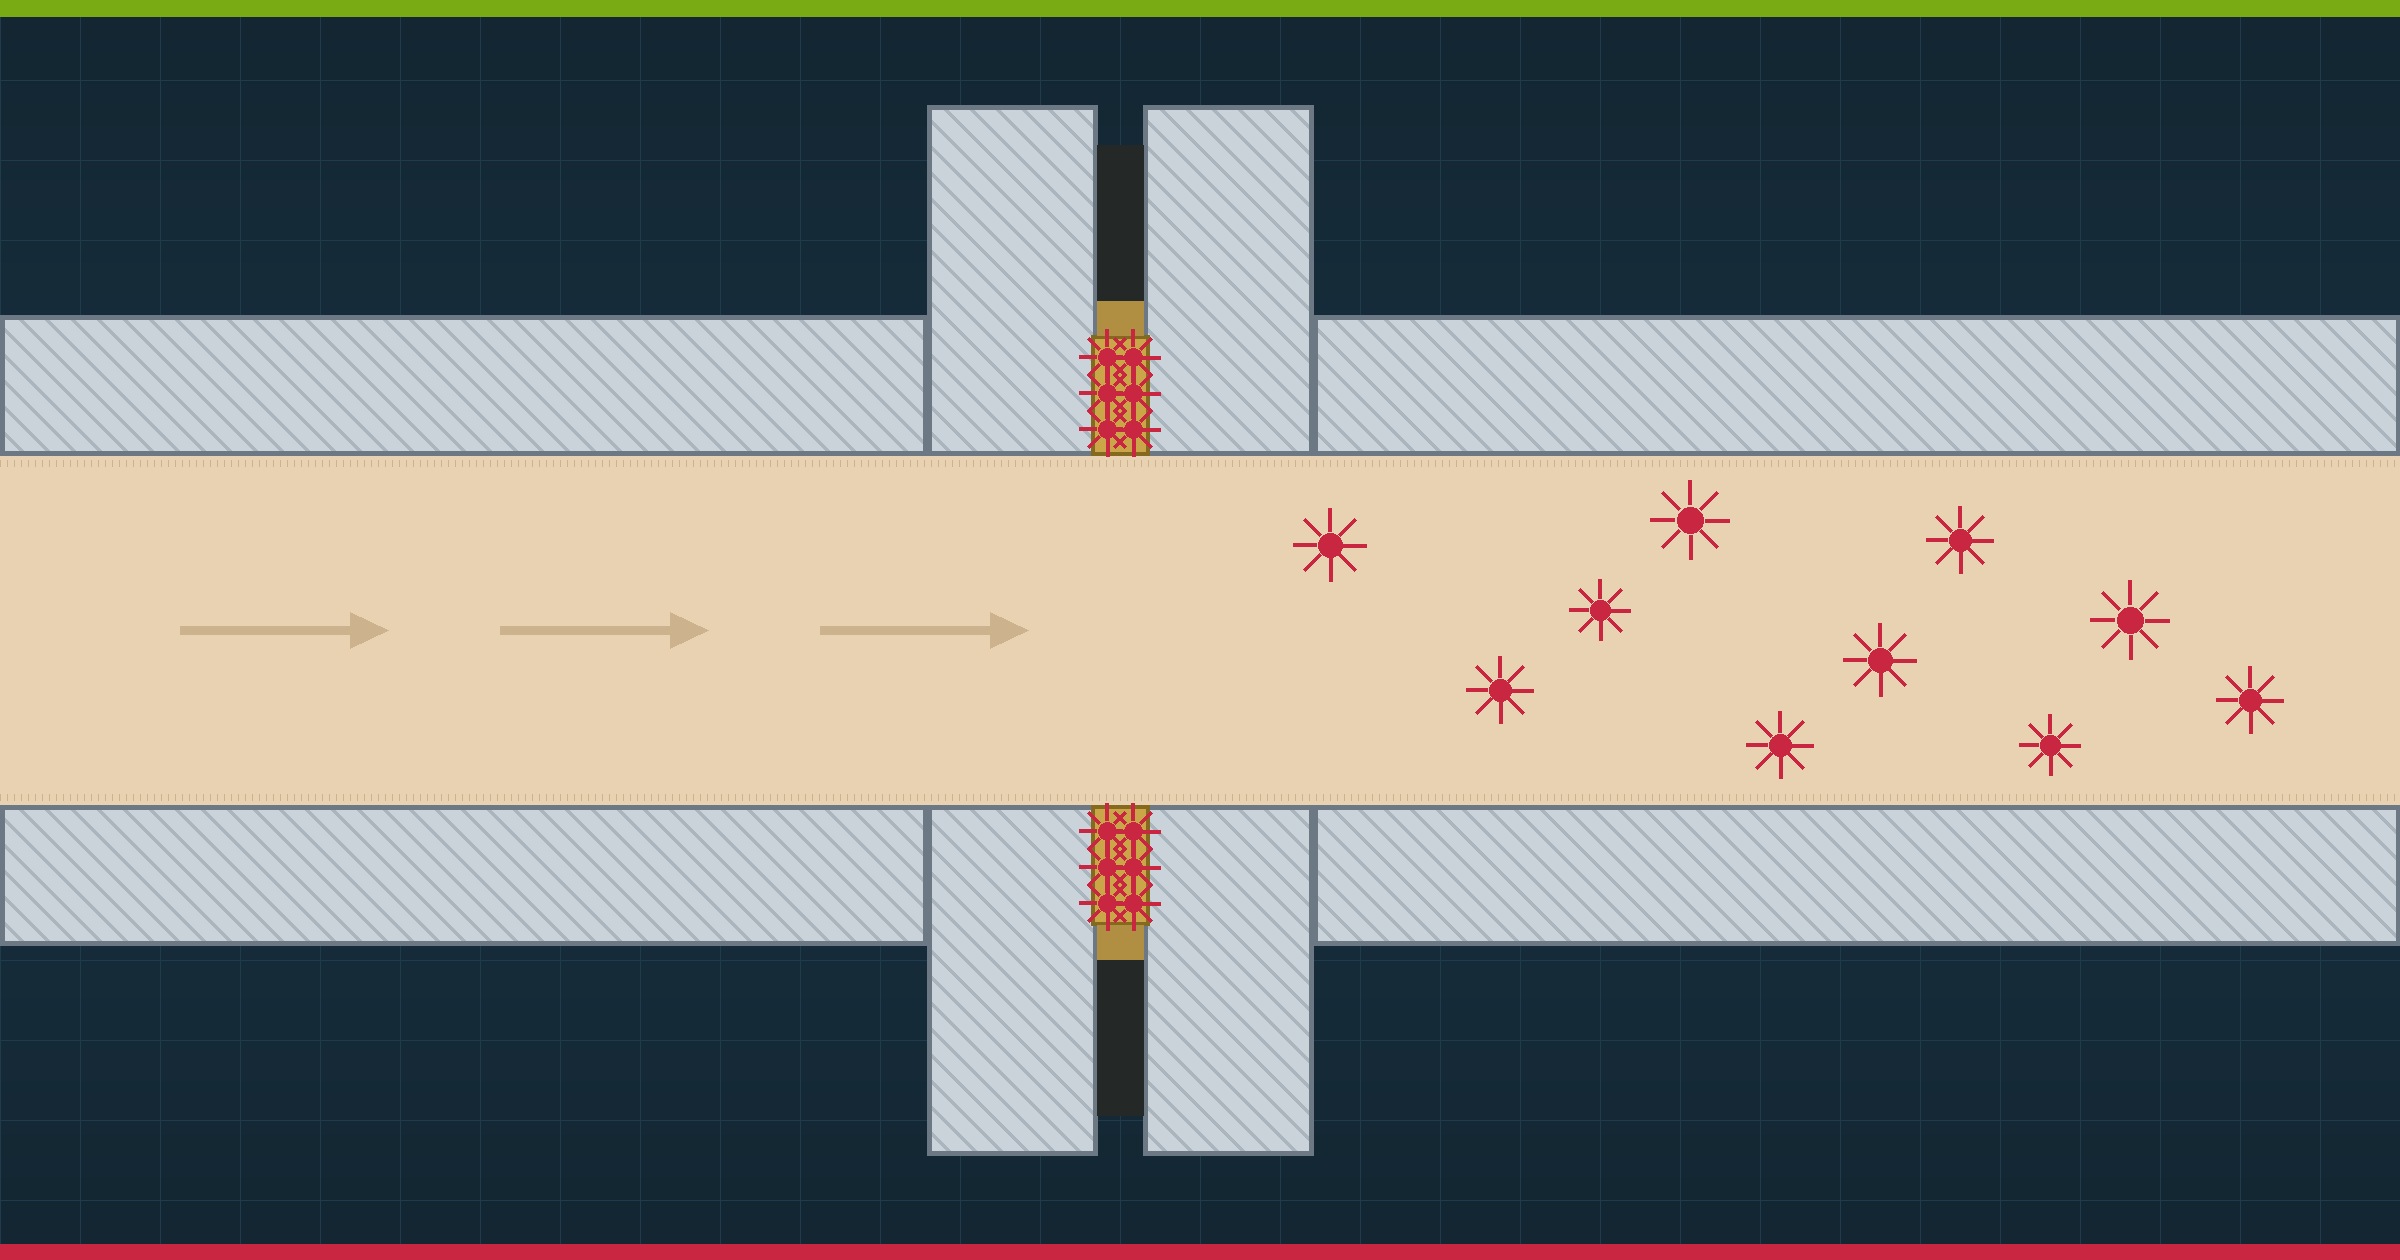
When it is not, the failure is always the same shape. An incomplete or intermittent weld leaves a crevice. The crevice holds product residue and rinse water through every clean, because chemistry and mechanical action stop at the mouth of a gap that narrow. A biofilm establishes, and organisms such as Listeria monocytogenes sit in that film, protected, releasing cells back onto the clean surface after every sanitation cycle. The swab keeps failing, the cleaning crew keeps getting blamed, and the actual fault is a few millimetres of missing weld metal that was bought and paid for years earlier.
That is why welding is not a fabrication detail. It is a food safety specification item, exactly like the grade of the steel or the fall of the floor.
What does a good hygienic weld look like?
You do not need to be a coded welder to hold a supplier to a standard. You need five sentences.
Continuous. The weld runs the full length of the joint with no stitches, skips or tack welding left exposed on the product side. An intermittent weld on a product contact surface is a hygienic design fault, full stop.
Fully penetrated. The weld metal reaches through the full thickness of the joint, so the inside of the tube shows a complete, even bead. Lack of penetration leaves an internal crevice you will never see without a borescope.
Smooth and flush. The internal profile is even with the parent material, with no sharp ridge, undercut or rough face. Where dressing is needed, it is ground and polished back to the specified finish, not painted over with sealant. Sealant on a weld is a confession.
Aligned. The two bores meet without a step. Misalignment leaves a ledge that collects soil on one side of the joint, and it is one of the most common findings when tube from two suppliers meets on site.
Purged. Stainless steel welded without inert gas shielding on the inside oxidises into a rough, sugary surface that corrodes early and cleans badly. Purging is a one line requirement in the specification and it costs almost nothing at fabrication stage.
Putting it in the purchase specification
The time to control weld quality is before fabrication starts, in the same document that states your steel grade and your surface finish. The lines are short. All product contact welds continuous, fully penetrated and crevice free. Internal weld profile smooth and flush, dressed where necessary to the specified surface finish, with a roughness average of 0.8 micrometres as the ceiling for product contact. Orbital TIG with internal purging on hygienic tube wherever the geometry allows a weld head. Every joint numbered on a weld map, every orbital weld logged, and material certificates supplied for the tube and fittings.
If you already have a specification format, these lines drop straight into it. If you do not, read how to write an equipment purchase specification that holds up at audit first, because weld requirements only have force when the rest of the document has force. EN 1672-2 and ISO 14159 give you the machinery hygiene language, EHEDG guidance covers welded joints on closed equipment, and 3-A practice does the same work in dairy. South African law sits underneath all of it: R638 regulation 6 requires food contact surfaces to be smooth, rust proof, non toxic, non absorbent and free of open joints or seams, and a crevice in a weld is exactly that, an open seam.
One specification, three courses, every number in its place
The Hygienic Design Pathway bundles Essentials, Intermediate and Food Safety for Engineering and Maintenance Teams. The ten rules, the materials and fabrication detail, and the same rules applied to repairs and modifications, in one enrolment.
Enrol in the Pathway, R6 337 →
Three courses, lifetime access. Saves R1 162 against the three at today’s prices.How do you inspect a weld you cannot see?
Internal weld inspection is a sampling exercise, and the sample is agreed before the first arc strikes, not negotiated afterwards. The specification states what percentage of product contact welds will be examined by borescope, who selects them, and that the buyer’s representative does the selecting. It states that a failed weld widens the sample. It states that the weld map, the weld log, the borescope images and the repair record come with the equipment as handover documents, and that the final payment waits for them.
At the factory acceptance test, pick your sample and look. On site, treat every site weld as a new joint that needs the same evidence, because installation welds are done in worse positions, under time pressure, often by a different contractor. The joint between two perfect machines is routinely the worst weld on the line.
When you find a bad weld in service, the repair is the same decision tree every time. If the joint is accessible, cut out or grind back and re weld, then dress and re polish to the specified finish. If it cannot be fixed now, it goes on the hygienic design risk register with a score, an interim control, an owner and a date. The free 30 point Hygienic Design Walk gives you the scored format to do that on the spot. What it never gets is silence. A known crevice on a product line is a finding an auditor will reach eventually, and the version of events where you found it first, scored it and planned the fix is a very different conversation from the version where they did.
Where to learn this properly
Welds are one module of a bigger discipline. Hygienic Design Essentials gives you the ten rules and trains your eye to find the faults, in five hours. Intermediate Hygienic Design goes into the metal: grades, welds, couplings, valves, tanks, and the CIP verification that proves the line cleans. Advanced Hygienic Design and Engineering turns it into a working site system, from specification to commissioning, over 24 hours at Level 5. All three were designed with industry leading engineers and technical food safety consultants, and all three come with lifetime access and a certificate.
Frequently asked questions
What is a hygienic weld on food equipment?
A weld that is continuous, fully penetrated, smooth and free of crevices, pits and misalignment on the product side. It leaves no gap, ledge or rough pocket where soil can sit and bacteria can grow. An intermittent or stitch weld on a product contact surface is a hygienic design fault by definition.
Why are welds a food safety risk?
Because a bad weld creates a crevice that cleaning cannot reach, on a joint that cannot be opened for inspection. Soil and moisture sit in the crevice, a biofilm establishes, and the point recontaminates the line after every clean. Unlike a gasket or a coupling, a weld cannot be unbolted, so the fault is permanent until it is cut out or reworked.
What is orbital welding and when should I ask for it?
Orbital welding is automated TIG welding in which the arc travels around the tube on a machine head under set parameters. It produces repeatable, full penetration welds with a consistent internal profile, which is why it is standard practice for hygienic tube in dairies, breweries and pharmaceutical plants. Ask for it on product contact pipework wherever access allows a weld head, and ask for the weld log that the machine records.
How do you inspect a weld inside a pipe?
With a borescope, on a sample of welds agreed before fabrication starts. The specification states the sample percentage, who selects the welds, and what happens when one fails. Pair the borescope sample with a weld map that numbers every joint, a weld log, and photographs of the internal profile, so the inspection can be traced joint by joint.
What surface finish should food contact welds and surfaces have?
The widely used ceiling for product contact surfaces is a roughness average of 0.8 micrometres, with welds dressed so they are smooth and flush with the parent material. Roughness above that holds soil and makes cleaning slower and less reliable. State the figure in the purchase specification rather than writing smooth, which a supplier can interpret.
Is a welded joint always better than a coupling?
For a permanent connection on a cleaned in place line, usually yes, because a correct weld has no gasket to age and no crevice to open up. Couplings belong where the joint must come apart for cleaning or maintenance. The wrong answer is a joint that is neither: a permanent coupling that is never opened, with a gasket nobody has seen since commissioning.
Stop buying problems you cannot see
Every weld on your next machine will be specified, inspected and documented, or it will be a surprise. Train the person who signs the purchase order.
Essentials, 5 hours, R2 400 Intermediate, 9 hours, R3 700 Advanced, 24 hours, R6 500
Lifetime access and a certificate on every course. Advanced is R6 500 until 30 November, then R7 900. Or take the three course Pathway for R6 337.Sources and further reading
- How to write an equipment purchase specification that holds up at audit
- 304, 316 or duplex? Choosing stainless steel for food equipment
- EHEDG Guideline 8: what it actually says
- EHEDG guidelines overview, ehedg.org
- The ASC hygienic design course series